

When choosing sunscreen packaging tubes, prioritize materials that offer UV resistance, air-tight seals, and BPA-free construction—especially if you're formulating or distributing skincare products. The best sunscreen packaging tubes balance product protection, user convenience, and environmental sustainability. Look for options with barrier linings (like aluminum or EVOH) to prevent ingredient degradation, and consider tube shape, nozzle design, and recyclability based on your target market’s needs. For brands focused on travel-friendly or eco-conscious consumers, lightweight, leak-proof, and recyclable laminate or PCR-plastic tubes are increasingly preferred 1.
About Sunscreen Packaging Tubes
Sunscreen packaging tubes are cylindrical containers designed specifically for storing and dispensing sunscreen lotions, creams, and gels. Unlike standard cosmetic tubes, these are engineered to protect light- and oxygen-sensitive ingredients commonly found in sun care formulations—such as avobenzone, zinc oxide, and octinoxate—which can degrade when exposed to UV light or air.
These tubes typically range from 0.5 oz to 6 oz in capacity and are used across consumer retail, travel kits, dermatological brands, and sample distribution. They’re popular among private-label skincare companies, startups, and contract manufacturers who need reliable, scalable packaging solutions that maintain product integrity over time.
Common applications include SPF 30–100 lotions, mineral-based sunblocks, after-sun gels, and children’s sunscreens. The right tube not only preserves efficacy but also enhances brand image through texture, print quality, and ease of use.
Why Sunscreen Packaging Tubes Are Gaining Popularity
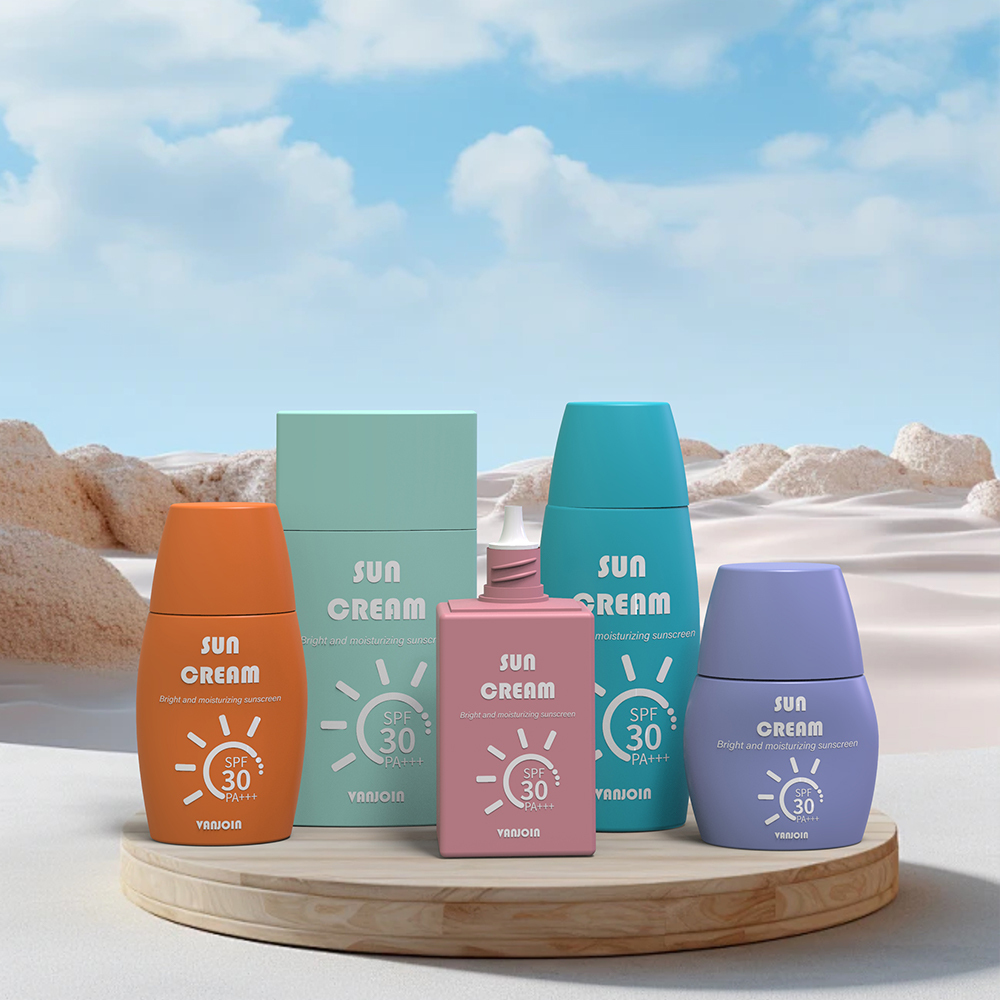
The demand for specialized sunscreen packaging tubes has surged due to several converging trends. First, global awareness of skin cancer and daily sun protection has driven higher SPF usage—even in non-beach contexts like urban commuting or driving 2. This shift increases the need for portable, reapplicable formats, making tubes ideal over jars or bottles.
Second, regulatory scrutiny around chemical stability has pushed brands toward packaging that extends shelf life. Degraded sunscreen loses its labeled SPF value, risking consumer safety and legal liability. High-barrier tubes help meet compliance standards by minimizing oxidation and photodegradation.
Third, sustainability concerns have accelerated innovation in recyclable and post-consumer resin (PCR) content tubes. Many brands now seek how to choose sunscreen packaging tubes that align with eco-certifications like Leaping Bunny or Zero Waste goals.
Finally, e-commerce growth favors compact, durable, and visually appealing designs. Tubes ship well, resist leakage during transit, and support full-body printing for branding—making them a top choice for DTC (direct-to-consumer) skincare lines.
Types and Variants of Sunscreen Packaging Tubes

Not all tubes are created equal. Understanding the differences between types helps match packaging to product chemistry and market positioning.
1. Laminated Aluminum Tubes
These multi-layer tubes combine plastic, aluminum foil, and inner lacquer to create a high-barrier seal against light, moisture, and oxygen.
- Pros: Excellent UV and oxygen protection; long shelf life; premium feel.
- Cons: Not widely recyclable; higher cost; limited flexibility in shape.
Ideal for high-end or medical-grade sunscreens with unstable active ingredients.
2. Plastic Laminate Tubes (PE + EVOH)
Made from polyethylene (PE) with an ethylene vinyl alcohol (EVOH) barrier layer, these offer strong protection while being lighter than aluminum.
- Pros: Good chemical resistance; more recyclable than aluminum; customizable shapes and colors.
- Cons: Barrier performance varies by EVOH thickness; may not suit highly sensitive formulas without additional lining.
A solid mid-range option for brands balancing performance and sustainability.
3. Monolayer HDPE or LDPE Tubes
Simpler single-layer plastic tubes made from high- or low-density polyethylene.
- Pros: Low cost; easy to recycle in many regions; suitable for short-shelf-life or mineral-only sunscreens.
- Cons: Poor UV and oxygen barrier; risk of ingredient degradation over time.
Best for budget-focused brands or samples/travel sizes where shelf life is under 6 months.
4. Recyclable & PCR-Content Tubes
These are typically HDPE or PP tubes made with 30%–100% post-consumer recycled plastic. Some are designed for mono-material recycling streams.
- Pros: Supports ESG goals; appeals to eco-conscious buyers; increasingly accepted in curbside programs.
- Cons: May have slight color variations; availability depends on supplier; slightly higher price.
Recommended for sustainable brands targeting Gen Z or millennial demographics.
5. Airless Pump Tubes
Equipped with a vacuum mechanism that prevents air from entering as product is dispensed.
- Pros: Maximizes preservation; reduces contamination; precise dosing.
- Cons: Expensive; complex manufacturing; harder to fill manually.
Suitable for luxury or clinical sunscreens with antioxidants or peptides added.
Key Features and Specifications to Evaluate
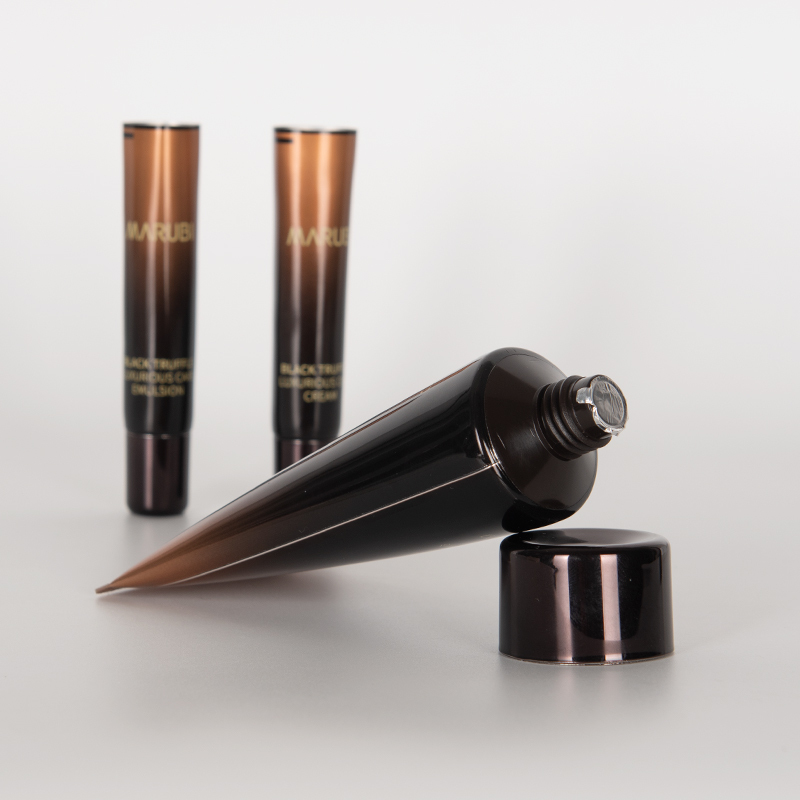
To make an informed decision on what to look for in sunscreen packaging tubes, assess these technical and functional criteria:
- Barrier Properties: Check for aluminum layers or EVOH barriers if using chemical UV filters. Request permeability test data from suppliers.
- Material Safety: Ensure tubes are BPA-free, phthalate-free, and FDA-compliant for cosmetic contact. Ask for Certificates of Compliance (CoC).
- Nozzle Design: Flip-top caps reduce spillage; wide mouths allow easier application; child-resistant caps add safety for family products.
- Printability: High-quality branding requires smooth surfaces compatible with offset, screen, or digital printing.
- Seal Integrity: Heat-sealed bottoms and crimped shoulders prevent leaks. Drop-test results should be available upon request.
- Capacity & Dimensions: Match tube size to intended use—travel (under 3 oz), daily (3–4 oz), or family (5+ oz).
- Sustainability Claims: Verify recyclability claims by checking local waste stream compatibility. Avoid “biodegradable” plastics unless certified compostable (e.g., TÜV OK Compost).
Pros and Cons: When to Use Sunscreen Packaging Tubes
Advantages:
- Prolongs sunscreen efficacy via superior ingredient protection.
- Portable and resealable—ideal for outdoor activities.
- Supports brand differentiation through custom design.
- Reduces product waste compared to jars (no double-dipping).
- Easier dosing control than spray formats.
Limitations:
- Higher upfront cost than jars or basic bottles.
- Recycling complexity—especially laminated or multi-material tubes.
- Filling requires specialized equipment for viscous formulas.
- Limited refillability, contributing to single-use waste unless part of a take-back program.
Tubes are best suited for brands prioritizing product stability, portability, and professional presentation. They’re less ideal for ultra-low-cost mass-market lines or refill-based circular models unless paired with innovative return systems.
How to Choose Sunscreen Packaging Tubes
Follow this step-by-step guide to select the optimal tube for your formulation and business model:
- Assess Your Formula Type: Is it chemical, mineral, or hybrid? Chemical sunscreens need high-barrier protection (aluminum or EVOH-lined). Mineral-only may work in monolayer HDPE.
- Determine Shelf Life Requirements: Products lasting over 12 months require better oxygen/light blocking. Request accelerated aging tests from suppliers.
- Define Target Market: Travelers prefer small, leak-proof tubes. Eco-buyers favor PCR or recyclable options. Luxury clients expect premium finishes.
- Evaluate Closure Options: Flip caps prevent accidental opening; screw caps offer tighter seals. Consider usability for elderly or arthritic users.
- Check Compatibility: Run a compatibility test by filling sample tubes and storing for 3 months under heat (40°C) and light exposure. Monitor for discoloration or odor changes.
- Review Supplier Credentials: Work with ISO-certified manufacturers. Ask about minimum order quantities (MOQs), lead times, and customization limits.
- Avoid These Red Flags:
- Suppliers who cannot provide material safety data sheets (MSDS).
- Vague recyclability claims without regional validation.
- No sample testing policy before bulk orders.
- Unrealistically low pricing—may indicate substandard lamination or thin walls.
Price & Market Insights
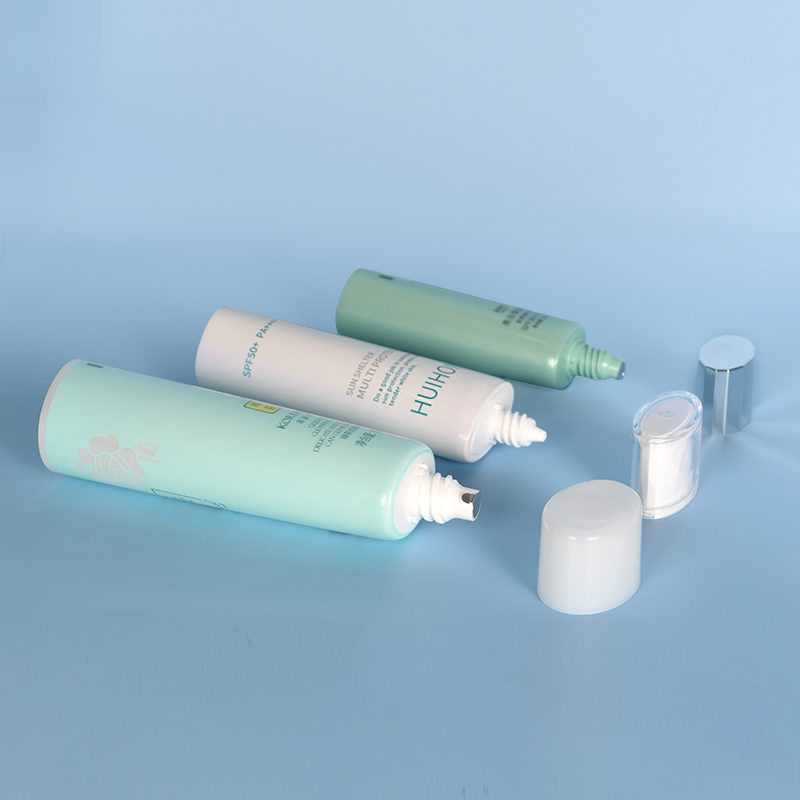
Pricing varies significantly based on material, quantity, and customization level.
- Monolayer HDPE: $0.15–$0.30 per unit (1,000–10,000 units).
- Laminated PE/EVOH: $0.40–$0.70 each.
- Aluminum laminate: $0.60–$1.20 each.
- Airless pump tubes: $1.50–$3.00+ depending on mechanism.
- PCR-content tubes: Add $0.05–$0.15 premium over virgin plastic equivalents.
Custom tooling (for unique shapes or nozzles) can cost $2,000–$8,000 one-time. MOQs typically range from 1,000 to 10,000 units for standard designs, lower for stock molds.
Value tip: For startups, consider buying pre-designed, recyclable HDPE tubes with minimal branding to reduce initial costs. Scale up to custom laminated options once market fit is proven.
| Type | UV Protection | Oxygen Barrier | Recyclability | Cost Range (per unit) |
|---|---|---|---|---|
| Laminated Aluminum | Excellent | Excellent | Poor | $0.60–$1.20 |
| PE + EVOH Laminate | Very Good | Very Good | Moderate | $0.40–$0.70 |
| HDPE (Virgin) | Fair | Poor | Good | $0.15–$0.30 |
| HDPE (30% PCR) | Fair | Poor | Good | $0.20–$0.35 |
| Airless Pump | Excellent | Excellent | Poor | $1.50–$3.00 |
Top-Seller & Competitive Analysis
Leading suppliers like Albea, Aptar, and Quadpack dominate the premium segment with advanced laminated and airless systems. Their tubes often feature:
- Custom shoulder and neck designs.
- Soft-touch coatings or matte finishes.
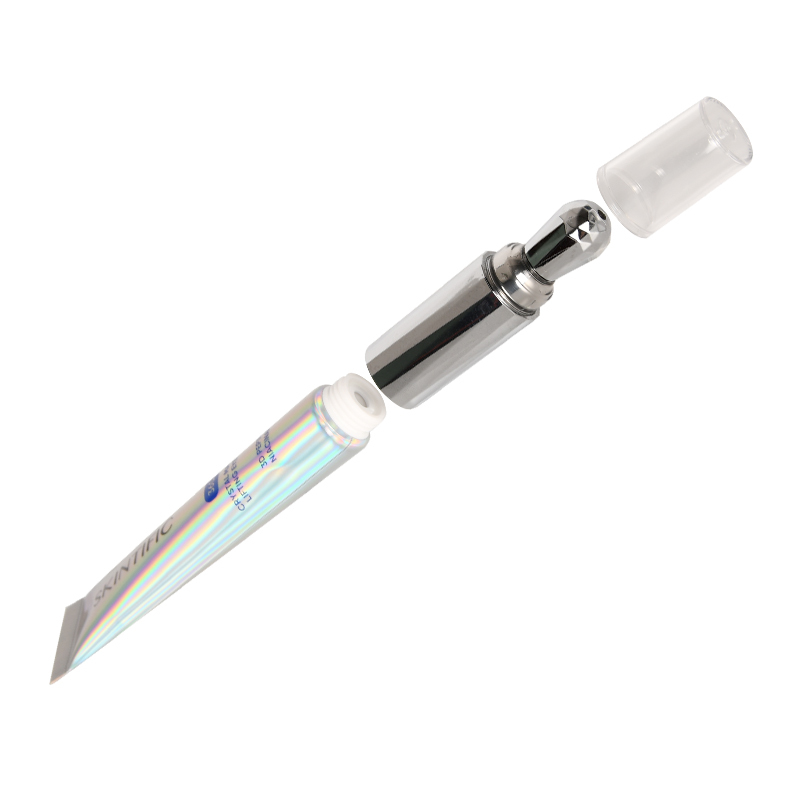
- Integrated applicator tips (e.g., brush or rollerball).
Mid-tier options from Chinese manufacturers (e.g., Cosmopak, PCL) offer competitive pricing on EVOH and PCR-HDPE tubes, though quality consistency may vary. Always request third-party lab reports for barrier performance.
When comparing top sellers, focus on total cost of ownership—not just unit price. A slightly more expensive EVOH tube might extend shelf life by 6 months, reducing returns and boosting customer satisfaction.
Customer Feedback Synthesis
Analysis of buyer reviews and industry forums reveals common themes:
Positive Feedback:
- “The flip cap prevents leaks in my gym bag.”
- “High-quality printing made our brand look professional.”
- “EVOH-lined tubes kept our SPF 50 stable for 18 months.”
Common Complaints:
- “Cheaper HDPE tubes let in light—product turned yellow.”
- “Difficult to squeeze out last bit; too much waste.”
- “Recyclability claim was misleading—local facility doesn’t accept laminated tubes.”
- “MOQ was too high for a small startup.”
These insights highlight the importance of matching tube specs to real-world usage and setting accurate sustainability expectations.
Sourcing & Supplier Tips
Whether buying wholesale or for private label, follow these guidelines:
- Start with Samples: Test at least 3–5 tube types with your actual formula before committing.
- Negotiate MOQs: Some suppliers offer reduced MOQs for first-time buyers or stock designs.
- Verify Certifications: Look for ISO 22716 (GMP), FDA registration, and recyclability certifications (e.g., How2Recycle).
- Consider Drop Shipping: Some B2B platforms (e.g., Alibaba, ThomasNet) connect brands with suppliers offering fulfillment services.
- Inspect Shipments: Randomly check filled tubes for leaks, seal defects, or printing errors upon delivery.
For U.S.-based production, domestic suppliers may offer faster turnaround and easier communication, though at higher cost. Overseas manufacturers (mainly in China, South Korea, and India) provide scale advantages but require careful vetting.
Maintenance, Safety & Legal Considerations
While tubes themselves don’t require maintenance, proper handling ensures product safety:
- Store filled tubes upright in cool, dark conditions to maximize shelf life.
- Avoid extreme temperatures during shipping to prevent expansion/leaks.
- Label tubes clearly with SPF value, active ingredients, expiration date, and usage instructions per FDA guidelines 3.
- Ensure child-resistant packaging if marketing to families—some states mandate this for certain formulations.
- Comply with regional regulations: EU requires CPNP notification; U.S. requires FDA facility registration.
Note: Packaging does not replace formulation stability testing. Always conduct full product testing under ICH Q1A–R2 conditions regardless of tube type.
Conclusion
Selecting the right sunscreen packaging tubes involves balancing protection, cost, usability, and sustainability. For most brands, EVOH-laminated or recyclable HDPE tubes offer the best compromise between performance and accessibility. Prioritize barrier properties if using chemical UV filters, and always validate supplier claims with real-world testing. Whether launching a new SPF line or optimizing an existing one, investing in high-quality, fit-for-purpose packaging improves both product efficacy and customer trust.
FAQs
What is the best material for sunscreen packaging tubes?
For maximum protection, laminated tubes with aluminum or EVOH barriers are best. For eco-friendliness, PCR-HDPE or fully recyclable mono-material tubes are recommended—depending on your formula’s sensitivity.
Are sunscreen tubes recyclable?
It depends on the material. Monolayer HDPE tubes are widely recyclable. Laminated tubes (plastic + aluminum) usually are not. Always check local recycling rules and label accordingly.
How do I prevent sunscreen from degrading in the tube?
Use high-barrier tubes (EVOH or aluminum), store away from light and heat, and ensure the cap creates an airtight seal. Conduct stability testing before launch.
Can I customize the shape and print of sunscreen tubes?
Yes, most suppliers offer custom tooling and full-body printing. Minimum order quantities apply, typically starting at 5,000–10,000 units for full customization.
What’s the typical shelf life of sunscreen in a tube?
Most sunscreens last 2–3 years unopened. Proper packaging extends stability. Once opened, use within 12 months for best efficacy. Mark expiration dates clearly on packaging.




 浙公网安备
33010002000092号
 浙B2-20120091-4